Strip-end preparation
Confirm how the previous strip tail and next strip head are cut or prepared, and what strip dimensions and materials the proposed equipment supports.
STRIP JOINING AT THE TUBE MILL ENTRY
Prepare and join the end of one strip to the start of the next coil during a coil change. XFX can discuss this entry-section equipment with a new ERW line or for an existing-line replacement.
The shearing method, joining scope and machine interfaces are confirmed for the actual strip and line. Partial information is enough to begin.
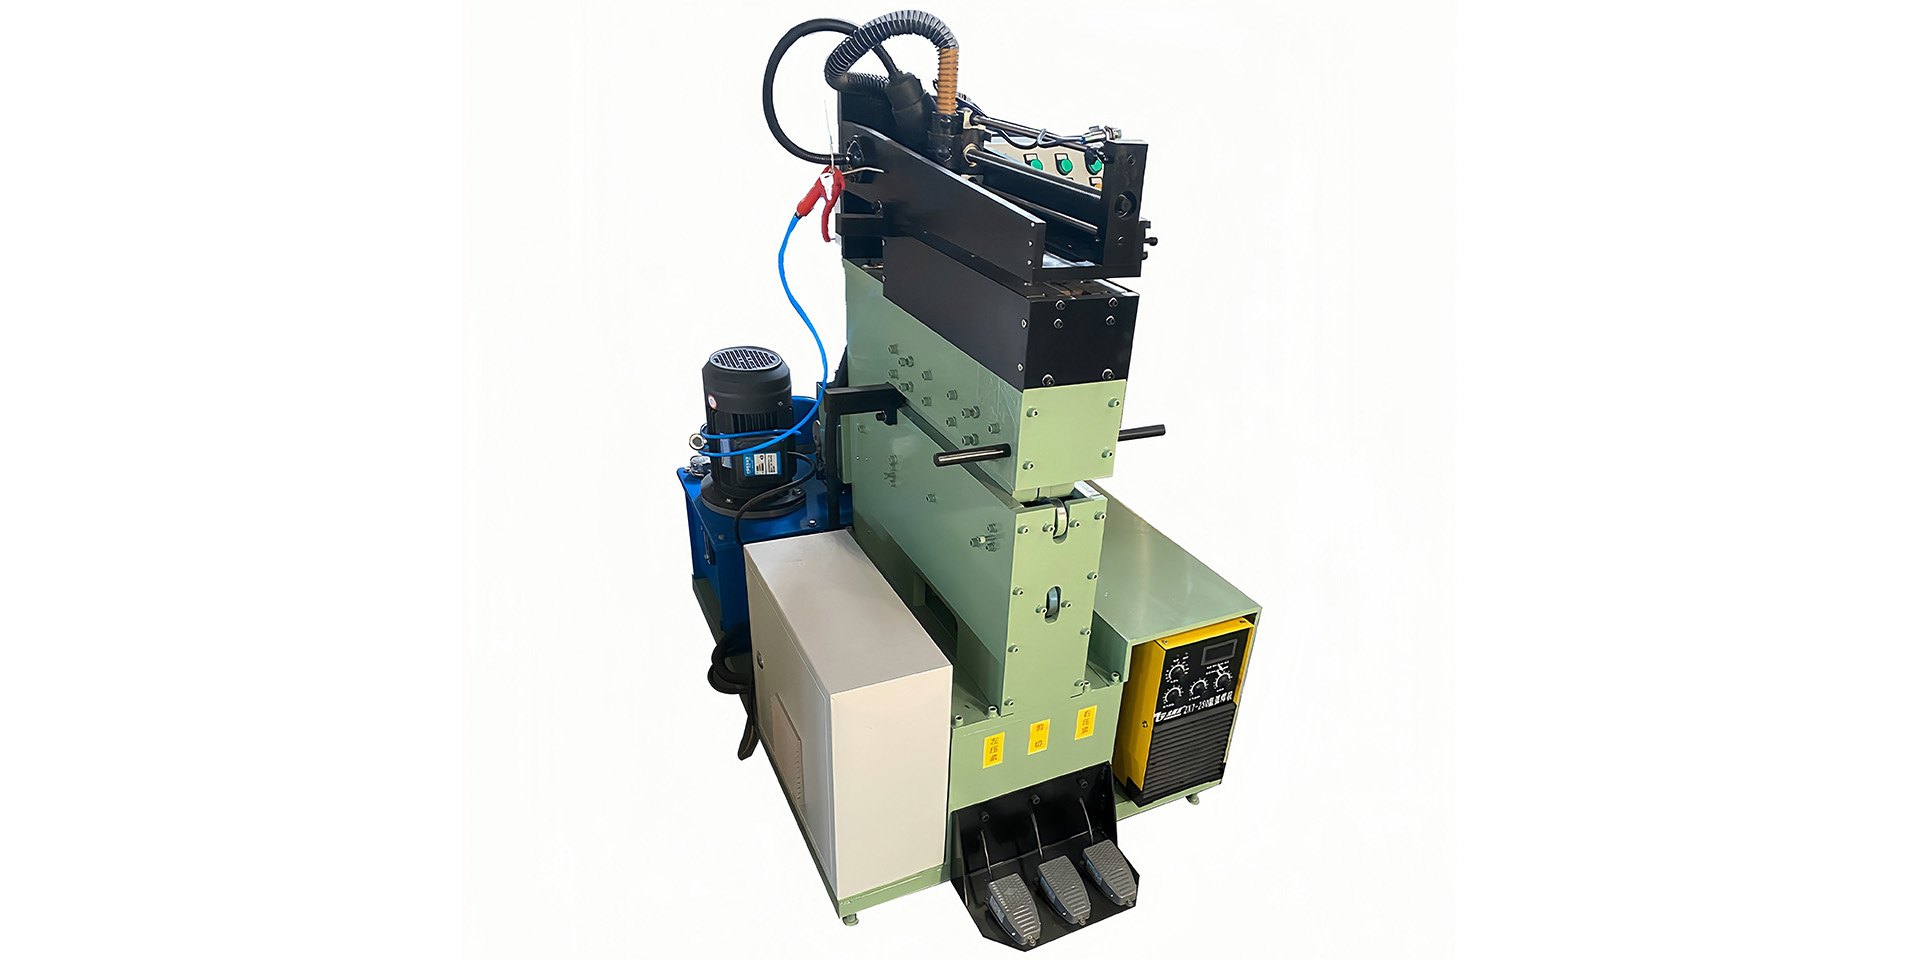
01 / THE PRODUCT ROLE
This equipment prepares the tail of the previous steel strip and the head of the next strip. In a shearing and butt-welding arrangement, the prepared ends are joined before the strip passes downstream.
The actual cutting and joining process, cycle timing and joint requirements must be reviewed for the proposed line and strip material.
02 / ENTRY-SECTION RELATIONSHIP
The machine is described after the uncoiler and before the accumulator. This sequence shows where to review the interfaces; it is not a list of automatically included machines.
Confirm mechanical, control and layout interfaces between the uncoiler, shearing/welding unit, accumulator and tube mill. Each machine’s supply scope belongs in the project proposal.
03 / SOURCE TERMINOLOGY & SCOPE
XFX describes shearing-only and shearing-and-welding equipment on the existing product page. Confirm the exact cutting and joining functions in the proposed configuration.
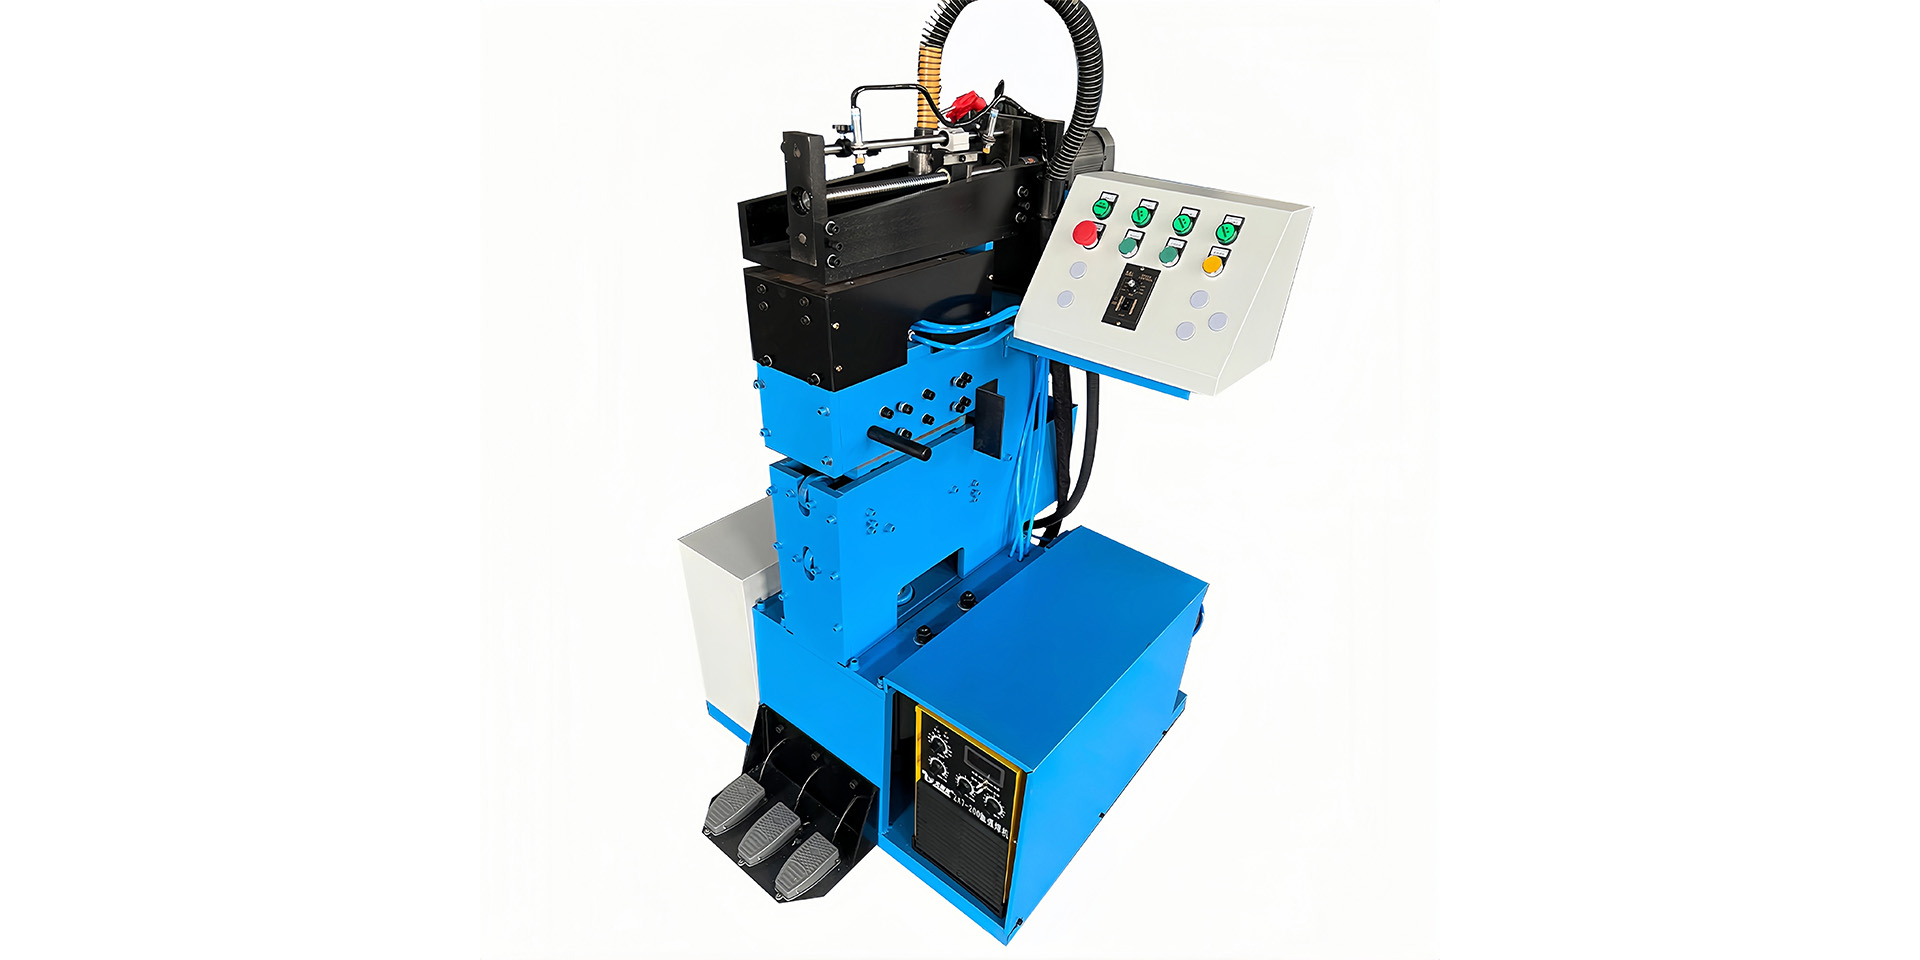
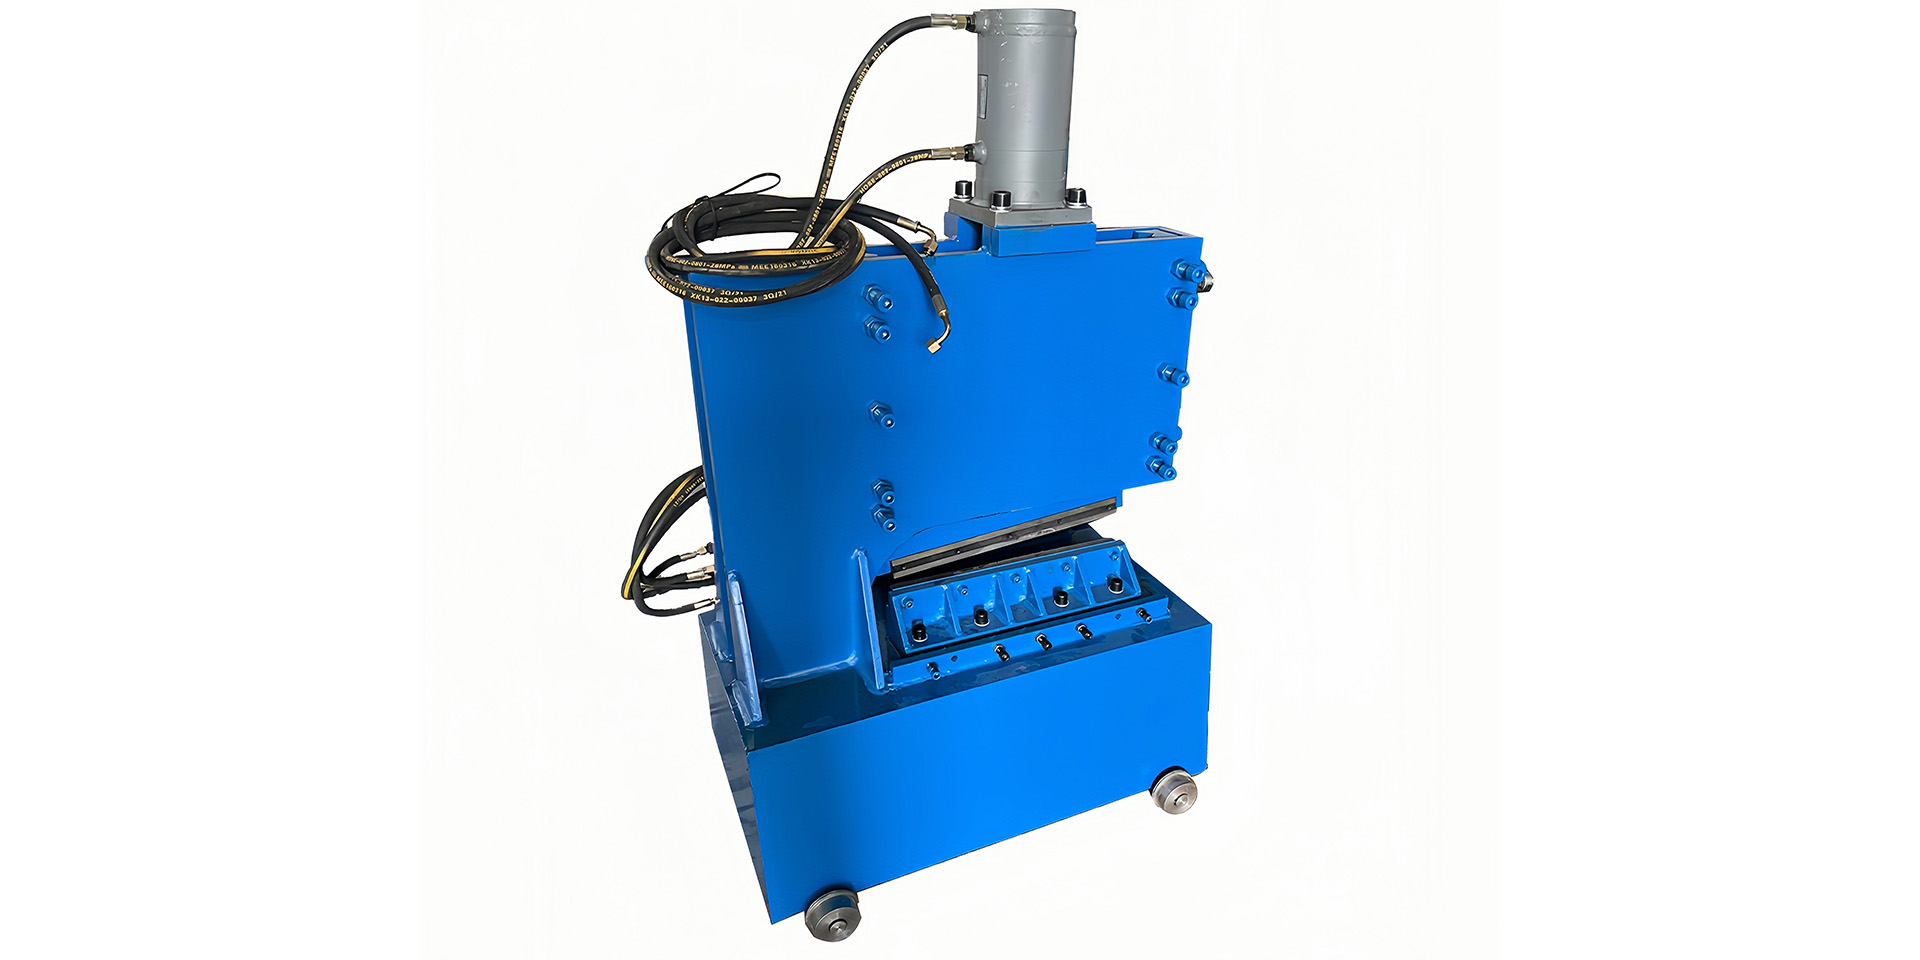
Ask XFX to confirm the supported strip values, utilities and operating requirements for the exact proposed configuration.
04 / SELECTION INFORMATION
Strip width and thickness need to be reviewed as a pair, along with material and the intended line. Send the products you know today; missing details can be discussed later.
Describe the raw strip material you plan to join.
List the actual widths to be processed.
Match each thickness to the relevant strip width.
Weight and inner/outer diameters if relevant and known.
Mill model or tube range, entry layout and accumulator plan.
Known line speed, coil-change frequency and utility conditions.
A tube diameter range by itself does not confirm the strip-end equipment. For final selection, XFX must review the actual strip products, joining method and line interfaces.
05 / TWO PROJECT ROUTES
Share the intended tube mill model or tube range, material, each strip width with its thickness, relevant coil details, expected output if known, entry layout, accumulator plan, electrical supply, pneumatic or hydraulic conditions where relevant, and destination country.
Uncoiler, shearing/welding, accumulator and tube mill scope should be listed separately in the proposal.
Discuss a new line ↗Send the existing mill and shearing/welding machine model, strip dimensions and grade, current joining method, layout, installation space, utilities, controls or interfaces, upstream uncoiler and downstream accumulator photos, and the current problem or upgrade goal.
Dimensions, strip range, mechanical interfaces, controls and utility requirements must be reviewed before a replacement solution is confirmed. No drop-in fit is promised.
Send existing-machine details ↗06 / QUOTATION REVIEW
This is a buyer checklist, not a standard-inclusion list.
The individual proposal states final supply, exclusions and any separate charges. No fixed operating time or weld-quality result is assumed here.
08 / FACTORY & SUPPORT
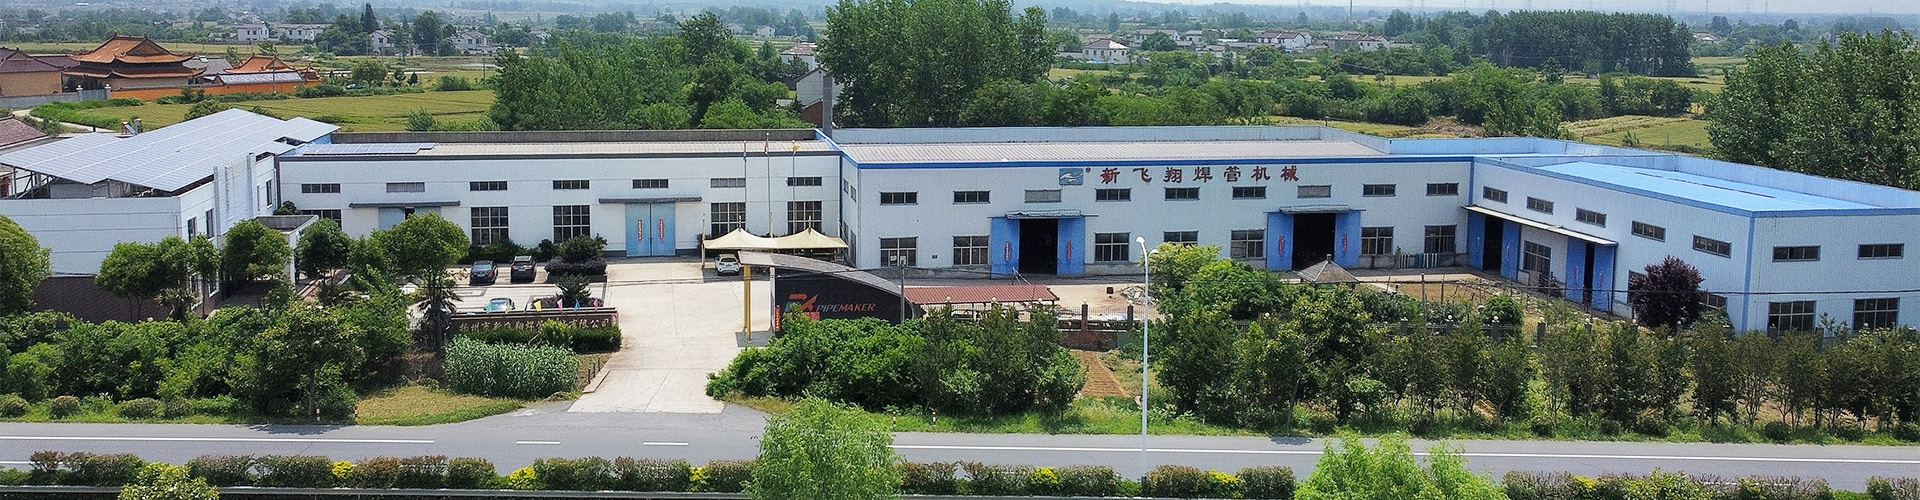
XFX has its own factory in China. For a project, XFX can provide on-site installation and commissioning, operator training, remote technical support, operation and maintenance documentation, and spare-parts support.
Overseas on-site arrangements and costs are confirmed in the individual proposal. No installation duration, technician count, response time or service price is stated here.
Contact XFX ↗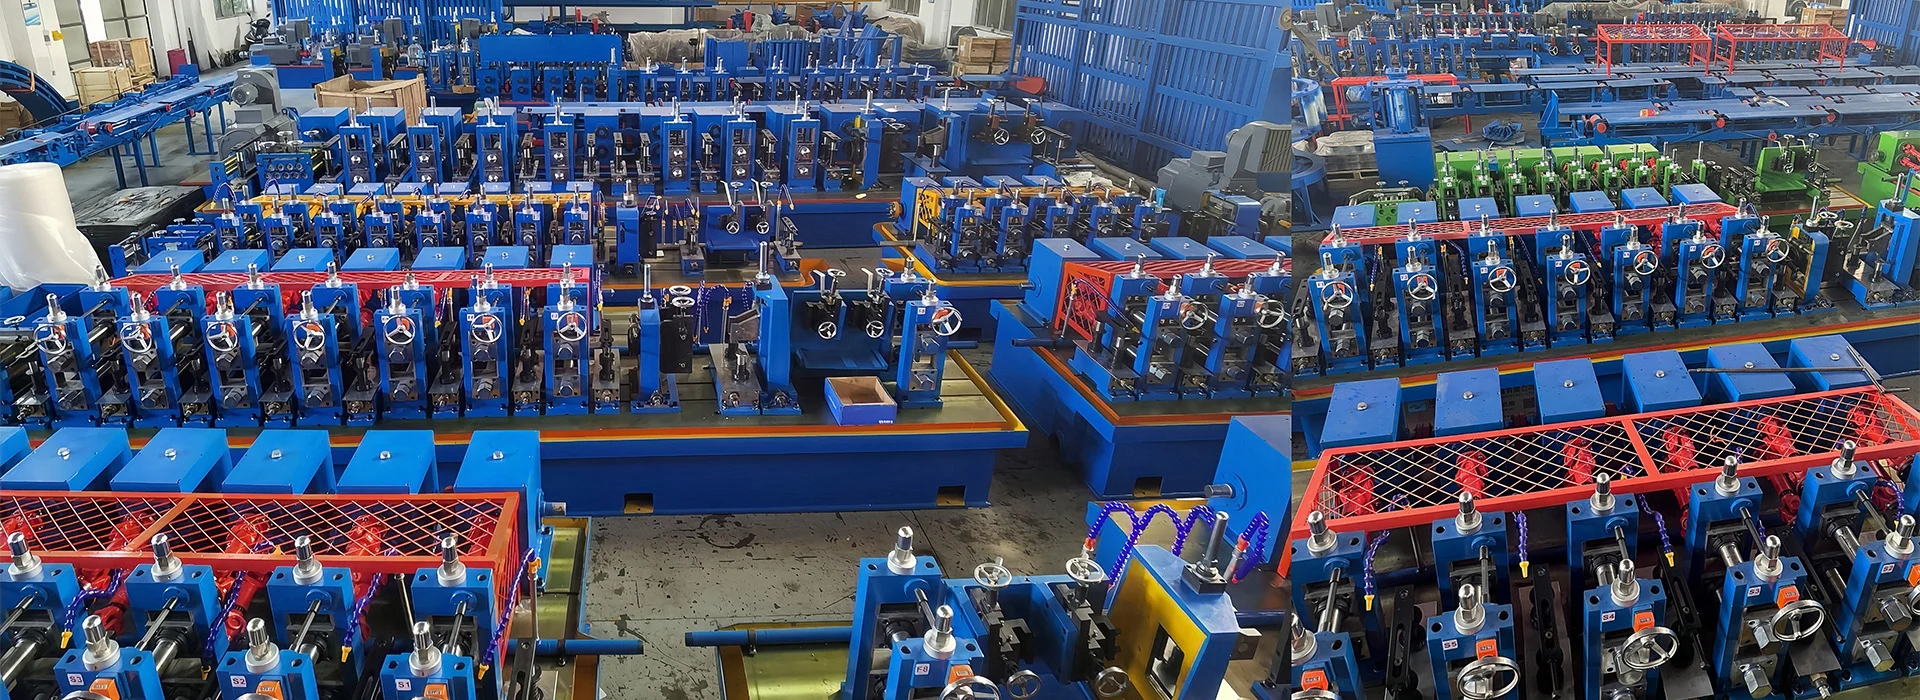
09 / BUYER QUESTIONS
The equipment prepares the previous strip tail and the next strip head. If the quoted arrangement includes butt welding, the prepared ends are joined before feeding strip downstream.
In the entry arrangement described by XFX, the next coil strip head is joined to the previous strip tail. The actual coil-change method depends on the proposed entry section.
Send material/grade and each actual strip width with its matching thickness. Add coil, tube mill, layout and line-speed information if known.
Yes. Share existing-machine photos, strip specifications, joining method, space, utility and control details, and photos of the uncoiler and accumulator. Compatibility must be checked before confirmation.
Do not assume so. Ask for an itemized proposal that states whether shearing, joining and related entry equipment are included.
It is positioned after the uncoiler and before the accumulator in the described line. Mechanical and control interfaces are reviewed for each project.
Project arrangements may include on-site installation and commissioning, training, remote support, operation and maintenance documents, and spare parts. Confirm the scope and overseas costs in the proposal.
10 / DISCUSS YOUR ENTRY EQUIPMENT
Tell us whether you need a new-line unit or an existing-line replacement. Share material, each strip width and thickness, and any layout or machine photos you have. You can begin with partial information.
View the Contact page ↗SEND AN INQUIRY
Use the message field for strip dimensions, material, new-line or replacement needs, and any existing-machine details.