Review the FX165 listing
See the separately listed round and square ranges, matching wall thicknesses and machine values for FX165.
View FX165 specificationsXFX ERW TUBE MILL LINES
FX165, FX219 and FX273 share one XFX listing but have separate round and square ranges, wall thicknesses, motor notations, HF welder values and listed speeds. Compare each model with your exact tube sizes and matching wall thicknesses before discussing a project configuration.
You can start with the specifications you already have. Final line selection needs a size-by-size review.
01 / THE LINE FAMILY
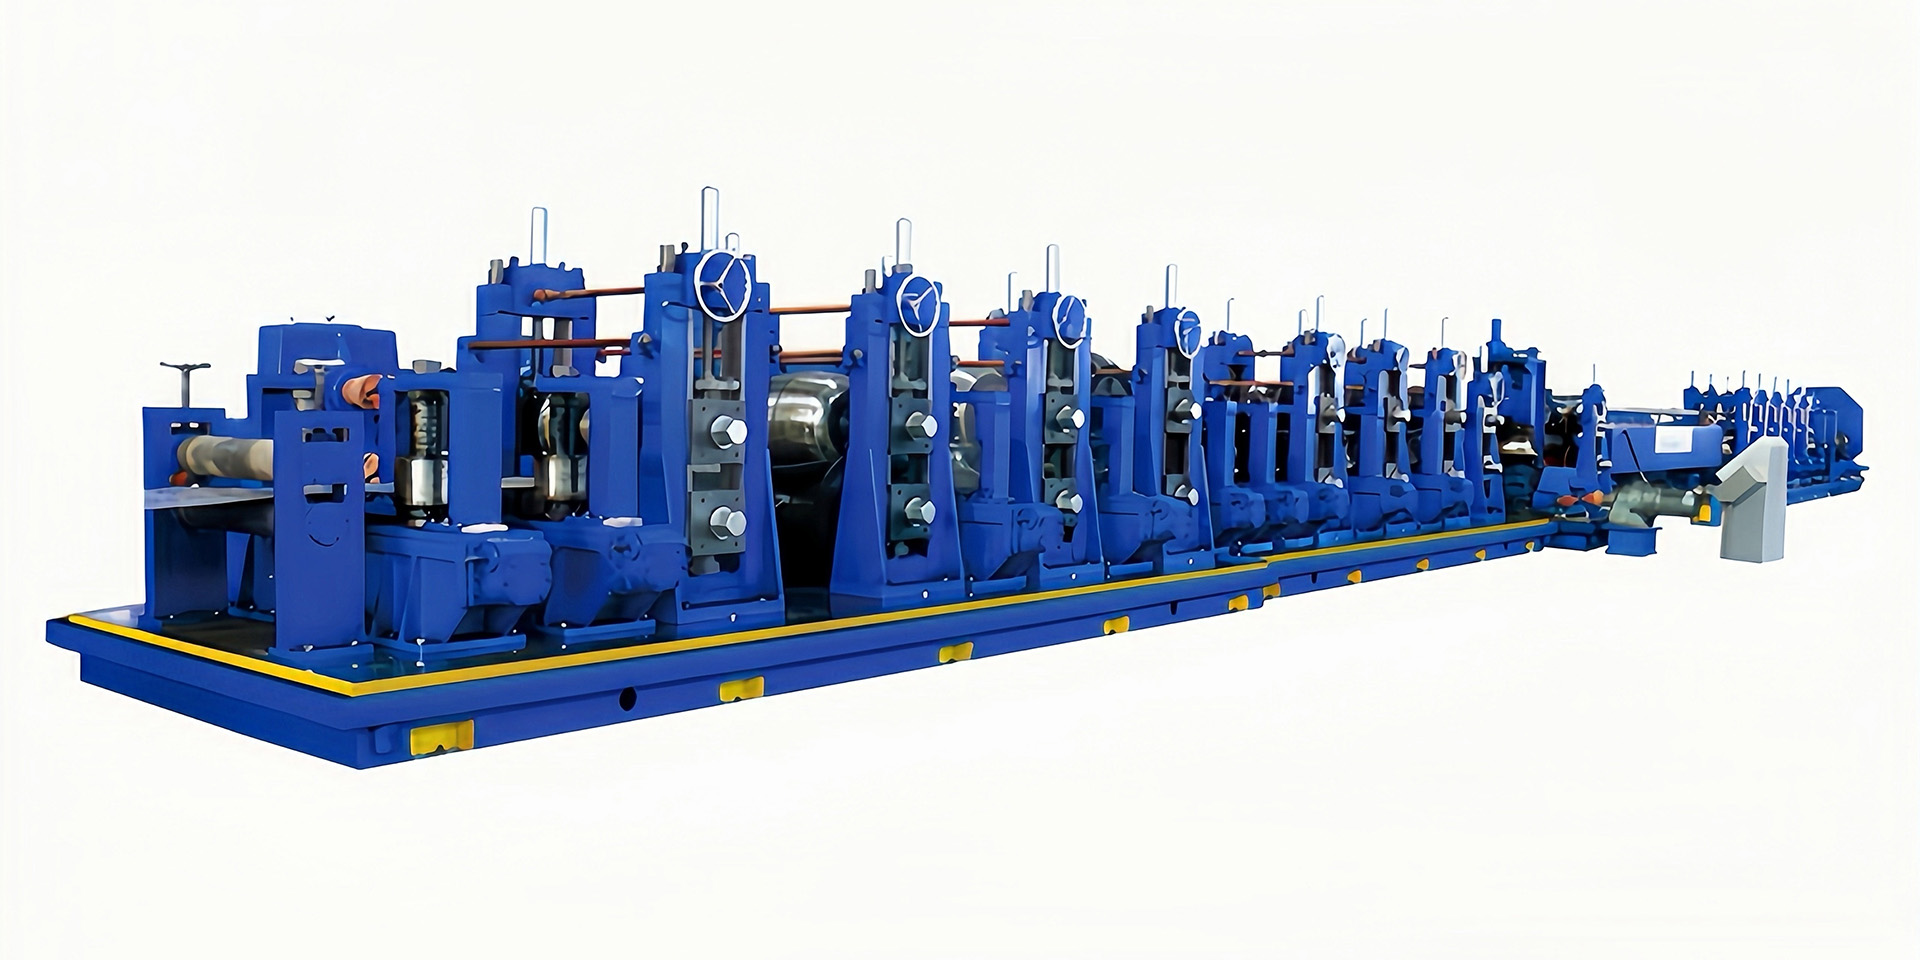
FX165, FX219 and FX273 share one XFX English product listing, with a separate technical column for each model. Review the three sections below, then send your complete tube schedule for a project-specific discussion.
An ERW line forms steel strip into tube, joins the longitudinal seam with high-frequency welding, sizes the section and cuts finished lengths. The appropriate equipment and tooling depend on your actual tube list, material and output target.
See the separately listed round and square ranges, matching wall thicknesses and machine values for FX165.
View FX165 specificationsSee the separately listed round and square ranges, matching wall thicknesses and machine values for FX219.
View FX219 specificationsSee the separately listed round and square ranges, matching wall thicknesses and machine values for FX273.
View FX273 specifications02 / TUBE SPECIFICATIONS
The saved XFX English product page lists these models in separate columns. Pair each planned tube size with its wall thickness; confirm line suitability and equipment scope in the project proposal.
FX165 / EXISTING SITE LISTING
FX219 / EXISTING SITE LISTING
FX273 / EXISTING SITE LISTING
The saved model table does not provide a model-specific rectangular-tube range. Send exact rectangular sections and paired wall thicknesses for review. A listed size and thickness range does not establish that every pairing is feasible. Listed speed is a reference from the existing XFX listing and is not a guarantee for every tube size, wall thickness or material combination. Final operating parameters are confirmed for the project. Main-motor notations are reproduced from the existing XFX listing without converting power or interpreting the drive configuration.
03 / PRODUCTION REQUIREMENTS
Round, square and rectangular tube projects may need different tooling and sizing arrangements. For each planned tube, pair the exact outside diameter or section size with its wall thickness. A broad size range on its own is not enough for final line selection.
You can contact us before every detail is settled. Tell us what is known now; we can identify what the technical proposal still needs.
Send your initial requirementsEven a partial schedule is useful for the first discussion.
04 / PRODUCTION PROCESS
A typical ERW route provides a way to discuss the line. Its exact stations and equipment scope are confirmed in the project proposal.
Additional seam treatment, cooling, packing and inspection needs should be specified for the project; this diagram is not a fixed bill of materials.
05 / EQUIPMENT SCOPE
The same product schedule can lead to different equipment choices. Confirm what is included, excluded or separately quoted before comparing offers.
Review coil handling, strip joining and how the line maintains strip supply during production.
Discuss the section mix, welding configuration, sizing method and controls for the required tube list.
Confirm finished lengths, end-quality expectations and the cutting and run-out arrangement.
Agree which sizes need tooling, how size changes will be handled and what spare-parts scope the project needs.
A cold saw, hot friction saw, accumulator type, uncoiler arrangement, packing equipment and tooling set are project decisions. No item above is promised as standard or free.
06 / TOOLING & SIZE CHANGES
Each tube shape and size change can affect roll tooling and setup. Share the sizes you expect to make most often and any future sizes that matter to your investment. XFX can then discuss a tooling plan with the line configuration.
Changeover time and the number of tooling sets are not assumed on this page; they belong in a project-specific technical proposal.
07 / FACTORY & SUPPORT
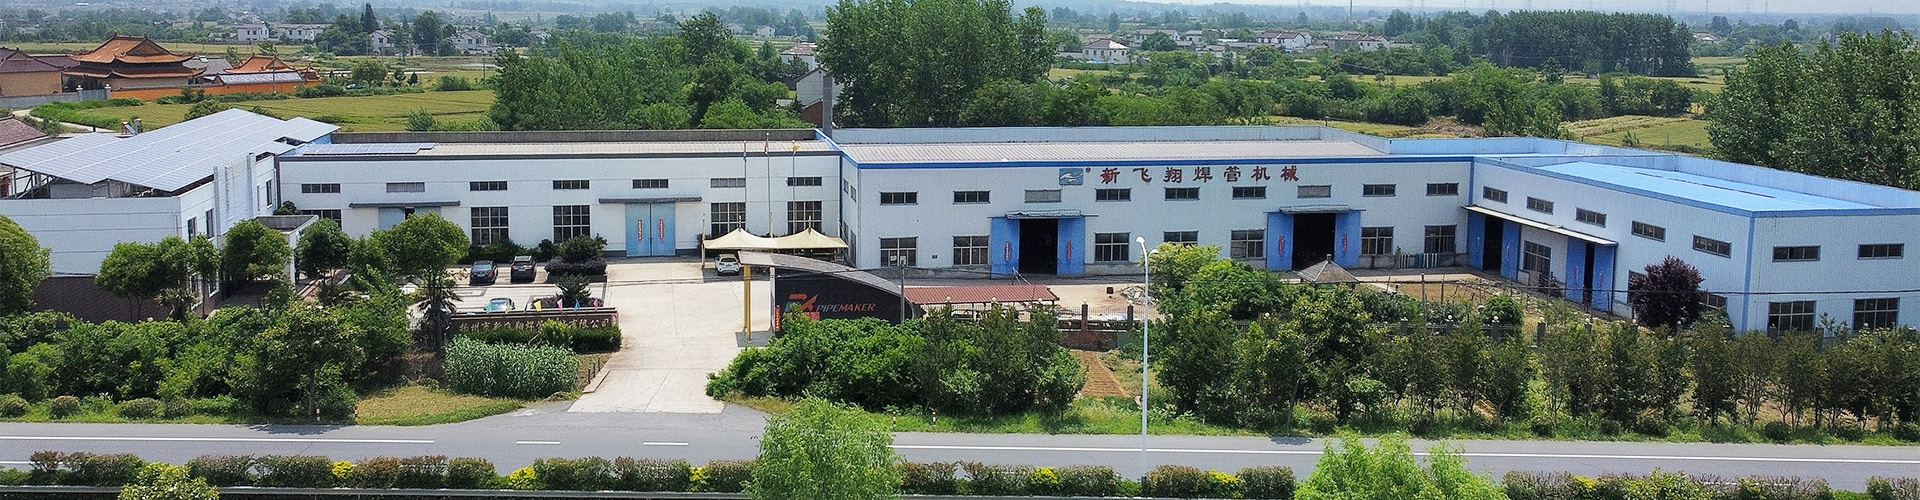
XFX has its own factory in China. We can provide on-site installation and commissioning, operator training, remote technical support, operation and maintenance documents, and spare-parts support.
The project's service scope is confirmed in its proposal. The customer is responsible for installation personnel's visas, flights, meals, accommodation and wages during the installation period.
Discuss support arrangements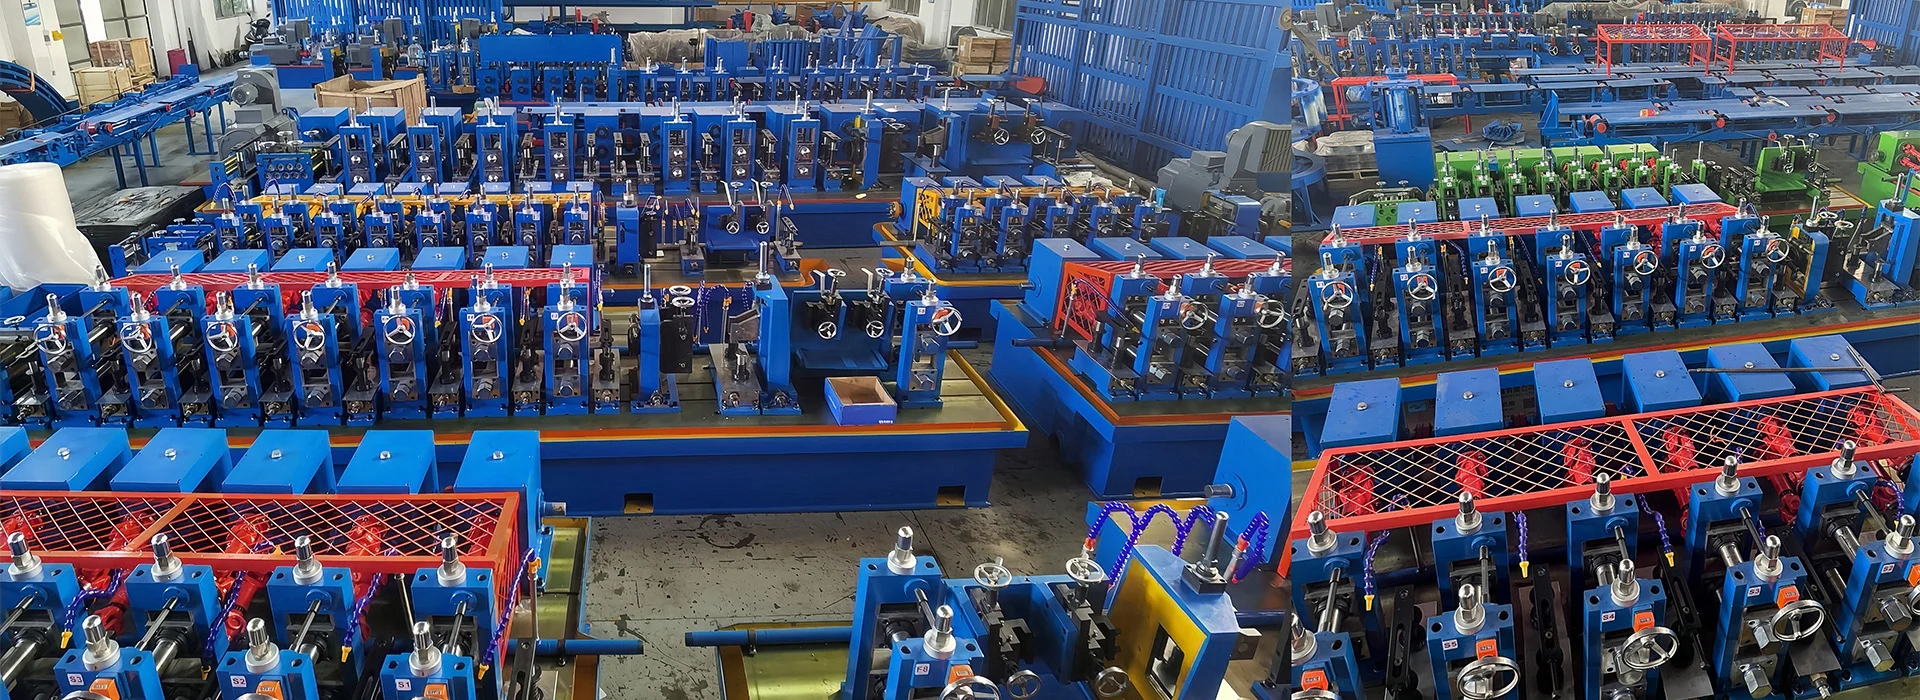
08 / BUYER QUESTIONS
Compare the separately listed round and square ranges, wall thicknesses, main-motor notations and HF welder values above. Ask XFX to review every planned tube size, matching wall thickness and material before confirming a line and tooling.
Yes. Start with what you know. For final line selection, each planned tube size should be matched with its wall thickness; material, output and cut length also help define the proposal.
The quotation should state the included equipment and any separately quoted options. Cutting method, tooling sets and packing arrangements are selected for the project, so do not assume a fixed package from a model name.
Yes. Send the exact section sizes and matching wall thicknesses. XFX can review the required forming, sizing and tooling arrangement before confirming feasibility for a particular model.
XFX can provide on-site installation and commissioning, training, remote technical support, operation and maintenance documents, and spare-parts support. Project details and the customer's installation-related costs are confirmed in the proposal.
09 / DISCUSS YOUR PROJECT
Send the shapes, exact sizes with their wall thicknesses, material and any output or cut-length target. You can start the conversation with partial information.
View the Contact pageSEND AN INQUIRY
Start with what you know. Include each tube size and its matching wall thickness where available.